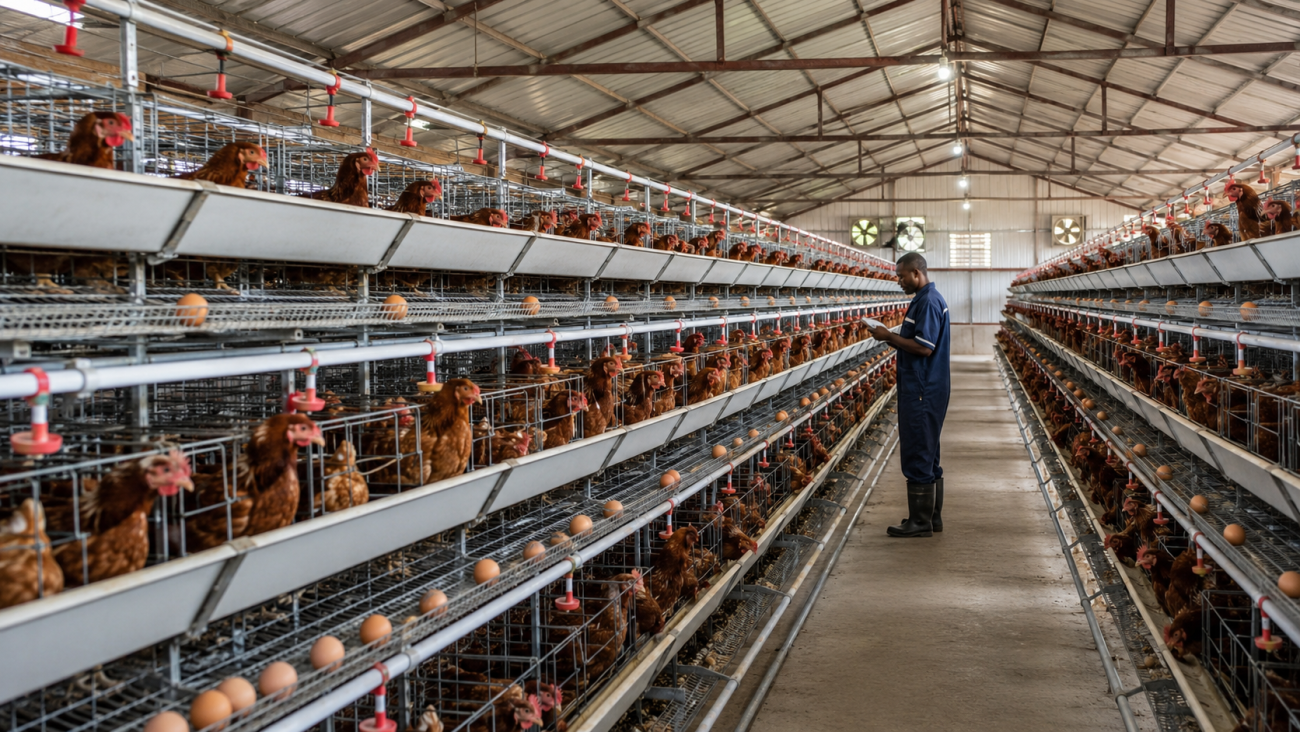
In the high-stakes world of commercial egg production, the difference between a profitable venture and a struggling farm often comes down to one thing: infrastructure efficiency. As global demand for eggs continues to rise, farmers are moving away from traditional floor-raised methods and outdated cage designs toward more sophisticated, automated solutions.
The H-Type Layer Cage System has emerged as the gold standard for large-scale operations. If you are looking to maximize your bird density, automate labor-intensive tasks, and ensure the highest hygiene standards, this system is your blueprint for success.

1. What is an H-Type Layer Cage System?
The H-Type layer cage system is a vertically stacked, multi-tier housing solution named for its “H” shaped steel frame. Unlike the A-type (pyramid) cages, where tiers are offset, H-type cages are stacked directly on top of one another.
This vertical alignment allows for the integration of advanced automation belts for manure removal and egg collection between each tier. It is essentially the “skyscraper” of the poultry world, designed to maximize the number of birds per square meter of land.
Key Structural Features:
High-Grade Galvanization: Most premium systems use hot-dipped galvanized steel to prevent corrosion from ammonia and moisture.
Multi-Tier Configuration: Typically ranging from 3 to 8 tiers high.
Integrated Belts: Each tier features a dedicated manure belt and egg collection track.
2. Why H-Type? The Benefits of Vertical Farming
When you’re managing 50,000 or 500,000 birds, every centimeter of space and every minute of labor counts. Here is why the H-Type system is the preferred choice for modern commercial poultry:
A. Maximized Land Utility
In traditional systems, land is often the biggest bottleneck. H-Type cages allow you to increase your bird capacity by 200% to 500% compared to floor-rearing or A-type systems within the same building footprint.
B. Superior Hygiene and Disease Control
Because the manure is removed instantly via PP (polypropylene) belts under each cage, the birds never come into contact with their waste. This drastically reduces ammonia levels in the air, lowering the risk of respiratory diseases and Coccidiosis.
C. Total Automation
The H-Type system is designed to be “hands-off.” From the moment the feed leaves the silo to the moment the egg reaches the packing room, the process is mechanized.
Reduced Labor Costs: One person can manage a house of 50,000 birds.
Precision Feeding: Automated trolleys ensure every bird gets the exact nutrient ratio, reducing feed wastage.
3. Core Components of the System
To understand how an H-Type system drives ROI, we need to look under the hood at the four main automated subsystems.
1. Automatic Feeding System
Modern H-type cages use either a Traveling Hopper (Trolley) or a Chain Feeding system. The trolley system is particularly popular because it distributes feed evenly across all tiers simultaneously, preventing the “first-bird-eats-all” scenario.
2. Automatic Nipple Drinking System
Hydration is key to egg size and shell quality.
360-degree Nipple Drinkers: Allows birds to drink from any angle.
Pressure Regulators: Ensures water pressure is consistent across high and low tiers.
Drip Cups: Keeps the manure belts dry, preventing bacterial growth.
3. Automatic Manure Removal (The “Game Changer”)
This is where the H-Type truly shines. A conveyor belt runs under each tier of cages. Every day (or several times a day), the belts move the manure to the end of the row, where a cross-conveyor takes it out of the building.
Pro Tip: Dry manure is much easier to sell as high-quality organic fertilizer, creating an additional revenue stream for your farm.
4. Automatic Egg Collection System
Egg breakage is a “profit killer.” The H-Type system uses soft, anti-static belts that gently transport eggs to a “lift” or “elevator” system. From there, they are moved to a central grading and packing area.
4. H-Type vs. A-Type: Which is Right for You?
Choosing between A-type and H-type is the most common dilemma for new poultry entrepreneurs.
| Feature | A-Type (Pyramid) | H-Type (Vertical) |
| Space Efficiency | Moderate | High |
| Automation Level | Basic to Semi-Auto | Fully Automated |
| Manure Removal | Scraper or Pit | Longitudinal PP Belt |
| Ventilation | Easy (Natural or Fan) | High-Tech (Tunnel Ventilation) |
| Initial Investment | Lower | Higher |
| Scalability | Limited | Exceptional |
The Verdict: If you have limited capital and a smaller flock (under 20,000 birds), A-type is a solid start. However, for Commercial Scale production (30,000+ birds), the H-type is almost always the better long-term investment due to labor savings and bird health.

5. Environmental Control: The “Closed House” Concept
You cannot put an H-type system in an open-sided shed. Because the bird density is so high, the birds generate a massive amount of body heat. To make an H-type system work, you need a Controlled Environment House (CEH).
Ventilation Requirements:
Tunnel Ventilation: Large exhaust fans at one end of the building pull air through cooling pads at the other end.
Cooling Pads: Use evaporative cooling to drop house temperatures by 5–10°C in hot climates.
Smart Controllers: Sensors monitor CO2, ammonia, temperature, and humidity, adjusting fan speeds in real-time.
6. Economic Analysis and ROI
Let’s talk numbers. Yes, the H-Type system requires a higher initial capital expenditure (CAPEX). However, the operating expenditure (OPEX) is significantly lower.
Feed Conversion Ratio (FCR): In a controlled H-type environment, birds waste less energy staying warm or cool. This improves FCR, meaning you spend less on feed to produce more eggs.
Egg Cleanliness: Automated collection results in a “Clean Egg Rate” of 98% or higher, allowing you to sell at premium market prices.
Mortality Rate: Better hygiene and climate control typically reduce mortality rates to below 5% over a laying cycle.
7. Best Practices for Maintenance
To ensure your H-type system lasts 15–20 years, follow these maintenance golden rules:
Daily: Check water pressure regulators and ensure manure belts are tracking straight.
Weekly: Lubricate the motor chains of the feeding and egg collection systems.
Monthly: Inspect the galvanized wire for any signs of wear or sharp edges that could injure the birds.
Post-Cycle: When the flock is cleared, perform a deep “wet-wash” disinfection of the entire steel structure.
8. Sustainability and Animal Welfare
The world is changing, and so is the poultry industry. Modern H-type cages are designed with Animal Welfare in mind.
Increased Space: Modern designs provide more “floor” space per bird to meet international standards.
Zinc-Aluminum Coating: This eco-friendly coating lasts longer than traditional galvanization, reducing the environmental footprint of the equipment.

Conclusion: Is the H-Type System Your Next Move?
Investing in an H-Type Layer Cage System is a commitment to the future of your poultry business. It transitions your farm from a traditional labor-intensive model to a data-driven, industrial-scale powerhouse. While the upfront costs are higher, the combination of land efficiency, bird health, and total automation ensures that your cost-per-egg remains the lowest in the market.
Ready to scale your egg production?
Would you like me to help you draft a customized Business Proposal or a Financial Projection for an H-type cage installation based on your specific flock size?