Introduction
The poultry industry is evolving rapidly, and efficient housing systems are at the heart of modern poultry farming. One of the most popular solutions for large-scale layer production is the H type chicken cage system. This cage design maximizes space utilization, ensures higher egg production, and reduces manual labor. Farmers worldwide are adopting this advanced cage system due to its efficiency, durability, and suitability for intensive poultry farming.
In this article, we will explore in detail: what an H type chicken cage is, its components, how it works, its key advantages, and essential maintenance tips. By the end, you will have a complete understanding of why the H type cage is an excellent investment for commercial poultry farms.
1. What is an H Type Chicken Cage?
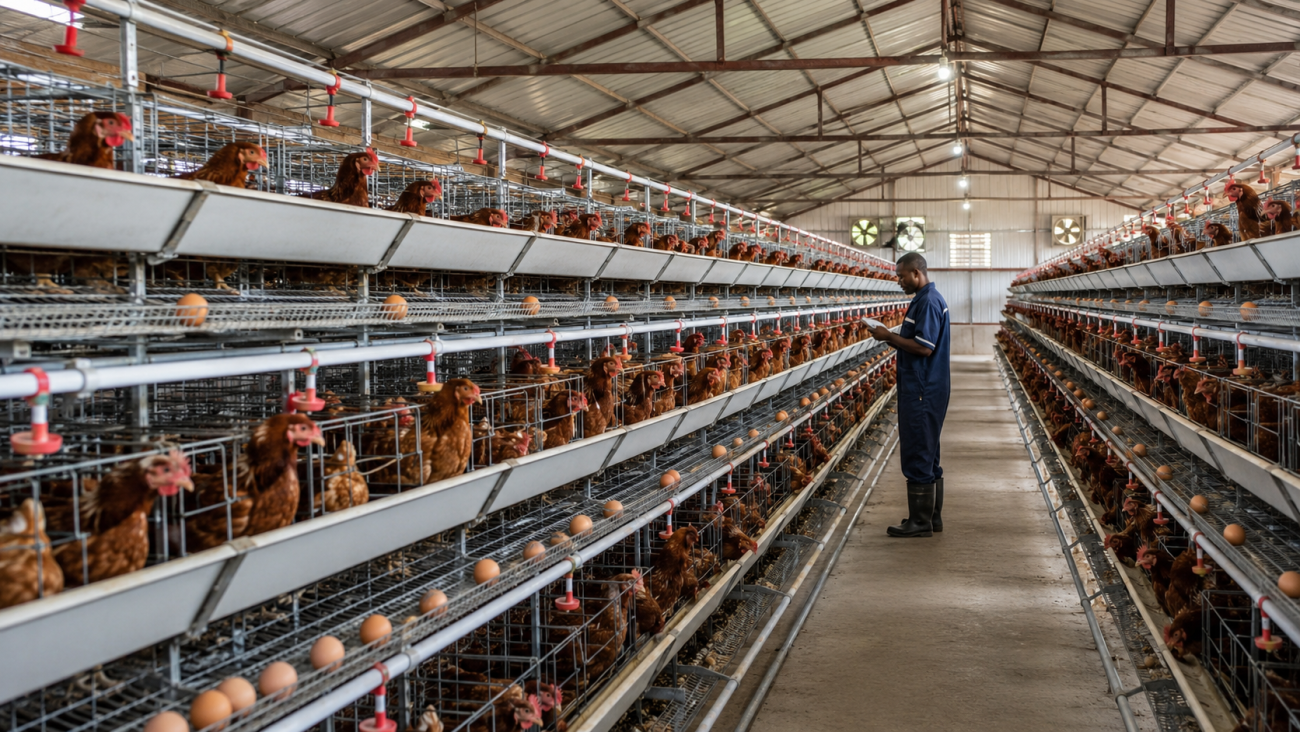
An H type chicken cage is a vertical, multi-tiered poultry cage system designed for layer hens, broilers, and pullets in intensive farming environments. The structure resembles the letter “H” when viewed from the front, hence the name.
Unlike traditional A-type cages, the H type system is more compact and allows higher stocking density without compromising bird welfare. It is widely used in large poultry farms across Asia, Africa, Europe, and South America because of its automated design that integrates feeding, drinking, egg collection, and waste removal.
The H type chicken cage is typically built with galvanized steel wire, ensuring strength, rust resistance, and a long service life. Depending on farm size and production goals, it can range from 3 to 10 tiers, housing tens of thousands of chickens in one building.

2. What are the Main Parts of an H Type Chicken Cage?
An H type chicken cage is a complete poultry housing system made up of several integrated components:
(a) Cage Frame and Wire Mesh
Constructed from hot-dip galvanized steel for durability.
Divided into tiers and compartments, with each cage holding 8–12 birds (depending on bird type and cage size).
Wire spacing is designed to prevent injuries while allowing manure and debris to fall through.
(b) Feeding System
Automatic feeding trolleys or chains deliver feed evenly to each tier.
Minimizes feed wastage and ensures uniform nutrition.
(c) Drinking System
Equipped with nipple drinkers connected to water pipelines.
Provides clean, fresh water on demand, reducing water spillage and maintaining hygiene.
(d) Egg Collection System
Automatic egg belts transport eggs gently from cages to a central collection point.
Reduces egg breakage and labor costs.
(e) Manure Removal System
Conveyor belts under each tier collect and transport manure outside the poultry house.
Helps maintain a clean environment and reduces ammonia buildup.
(f) Ventilation and Lighting System (Optional)
Many farms combine H type cages with mechanical ventilation and LED lighting systems.
Enhances bird comfort and supports optimal egg-laying cycles.
3. How Does the H Type Chicken Cage Work?
The working principle of the H type cage system lies in automation and systematic management:
Feeding – Feed is distributed automatically by the feeding trolley to each cage row. Birds can access feed equally, which improves growth and egg production.
Drinking – The nipple drinker system ensures birds always have access to clean water, which is essential for health and egg quality.
Egg Collection – As hens lay eggs, they gently roll onto the egg belt. The conveyor moves eggs to a central point, where they are collected, graded, and packed.
Manure Removal – Droppings fall onto manure belts beneath the cages. The belts transport waste outside, keeping the poultry house clean and reducing disease risks.
Ventilation and Lighting – Fans and lights regulate temperature, humidity, and day-night cycles, creating a comfortable environment for birds.
Through this fully integrated system, farmers can manage thousands of chickens with minimal manual labor while maintaining high efficiency and productivity.
4. What are the Advantages of H Type Chicken Cages?
The H type chicken cage system offers multiple benefits for commercial poultry farms:
(a) High Stocking Density
Maximizes the use of vertical space.
Ideal for large-scale farms aiming to raise 10,000–100,000 birds or more in one house.
(b) Labor and Cost Efficiency
Automation reduces the need for manual feeding, watering, and egg collection.
Lowers operational costs and improves management efficiency.
(c) Better Egg Quality and Production
Automatic egg collection reduces breakage rates.
Clean environment ensures hens remain healthy, which leads to higher laying rates.
(d) Improved Hygiene and Disease Control
Manure removal belts prevent droppings from accumulating under cages.
Lower ammonia levels reduce respiratory problems and disease outbreaks.
(e) Durability and Long Lifespan
Made from galvanized steel, resistant to rust and corrosion.
Can last 15–20 years with proper care, making it a cost-effective investment.
(f) Environmentally Friendly
Manure can be easily collected and processed into organic fertilizer.
Helps reduce environmental pollution.
5. Maintenance and Care Tips for H Type Chicken Cages
To ensure long-term efficiency and durability, regular maintenance of the H type cage system is essential. Here are some best practices:
(a) Cleaning and Disinfection
Clean cages, feeders, and drinkers regularly to prevent bacterial buildup.
Disinfect the poultry house between flocks to reduce disease risks.
(b) Check Feeding and Drinking Systems
Inspect feeders and nipple drinkers to ensure they are not clogged or leaking.
Calibrate feed trolleys to distribute feed evenly.
(c) Egg Belt and Manure Belt Maintenance
Check conveyor belts for wear and tear.
Lubricate moving parts and replace damaged belts promptly.

(d) Wire Mesh and Frame Inspection
Look for signs of rust, bending, or wire breakage.
Repair or replace damaged sections to prevent bird injuries.
(e) Ventilation and Lighting
Clean fans and check motor functions regularly.
Replace faulty bulbs and ensure lighting schedules are consistent.
(f) Professional Servicing
Schedule periodic inspections from the equipment supplier.
Upgrading parts such as motors and control panels extends equipment life.
Conclusion
The H type chicken cage system has transformed modern poultry farming by combining high stocking density, automation, and efficient waste management. It not only improves egg production but also reduces labor costs and enhances bird welfare.
By understanding its structure, working principle, and advantages, farmers can make informed decisions when investing in poultry housing equipment. Moreover, proper maintenance and regular servicing will ensure the cage system lasts for many years, delivering excellent returns on investment.
For commercial poultry farmers aiming for higher efficiency and profitability, the H type chicken cage is undoubtedly a smart choice.